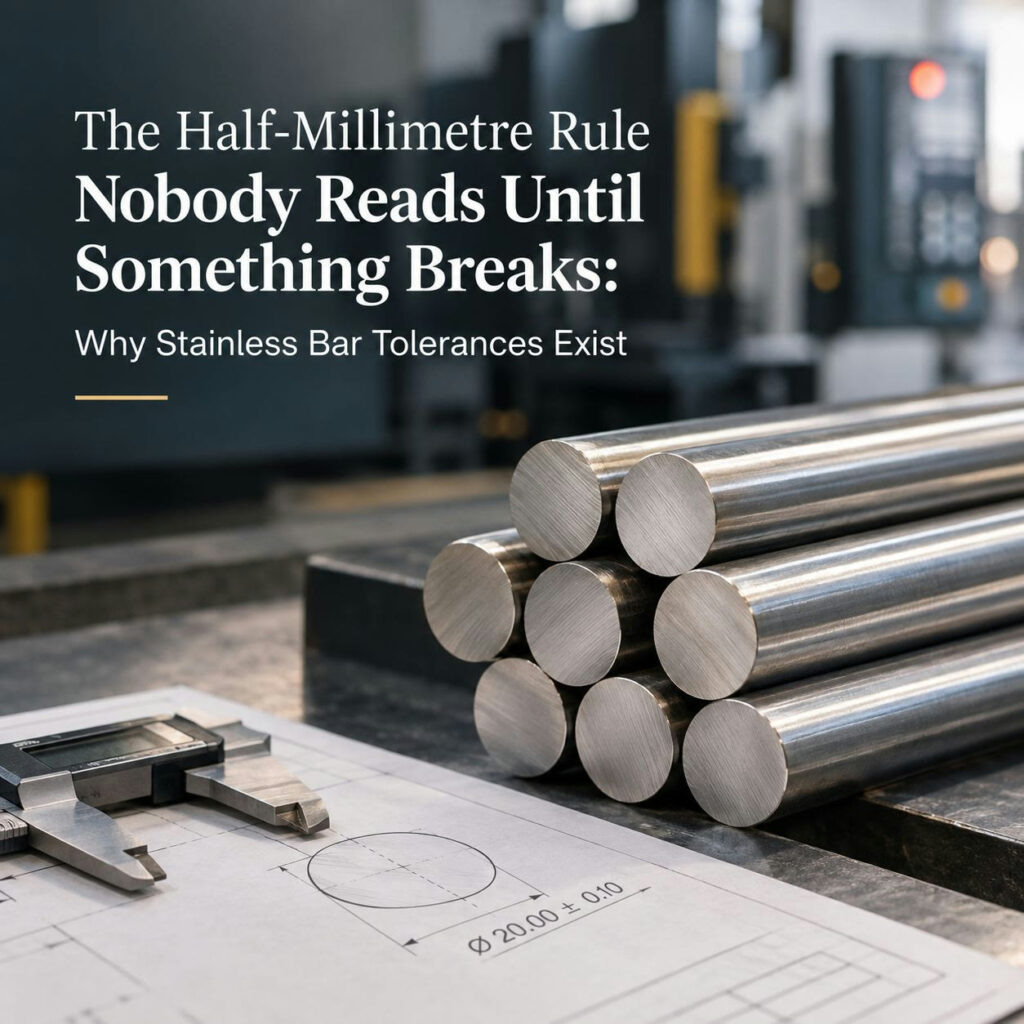
Dimensional tolerance classes (h8 through h11 and beyond, per DIN 671 / ASTM A484) define the permitted deviation from nominal diameter along a bar’s length. Tighter classes cost more to produce — more passes, slower feed rates, higher rejection risk — so specifying tighter than the application actually requires is a common and avoidable source of overspend.
h11 / h11a — general purpose
The widest common tolerance band, suited to components that will be substantially machined to final size regardless of incoming bar tolerance — structural work, general fabrication, parts where the bar diameter itself isn’t a functional dimension.
h9 / h10 — standard precision
A reasonable middle ground for components with moderate size-critical requirements — bushings, standard fasteners, parts fed through automated bar-stock machines where consistent diameter reduces machine setup and scrap.
h8 and tighter — high precision
Reserved for applications where the bar’s own diameter is close to a functional final dimension — precision shafts, components with minimal machining allowance, high-speed automatic lathe work where variation in stock diameter directly affects cycle time and tool wear.
A practical approach
Work backward from your process: if the bar will be turned down significantly before use, a looser (and cheaper) tolerance class rarely matters. If your machine feeds directly from bar stock with minimal stock removal, tolerance class becomes a real cost-and-quality lever worth specifying carefully. When you send us a drawing, our team will flag if the tolerance called out is tighter than the application appears to need — it’s a five-minute conversation that can meaningfully change your per-piece cost.